Protect multimillion-dollar wafer lots from mechanical equipment failure: Low-noise vibration surveillance and wideband acoustic audio emission monitoring for turbomolecular vacuum pumps, Chemical Mechanical Planarization (CMP) tools, and cleanroom air handling infrastructure.
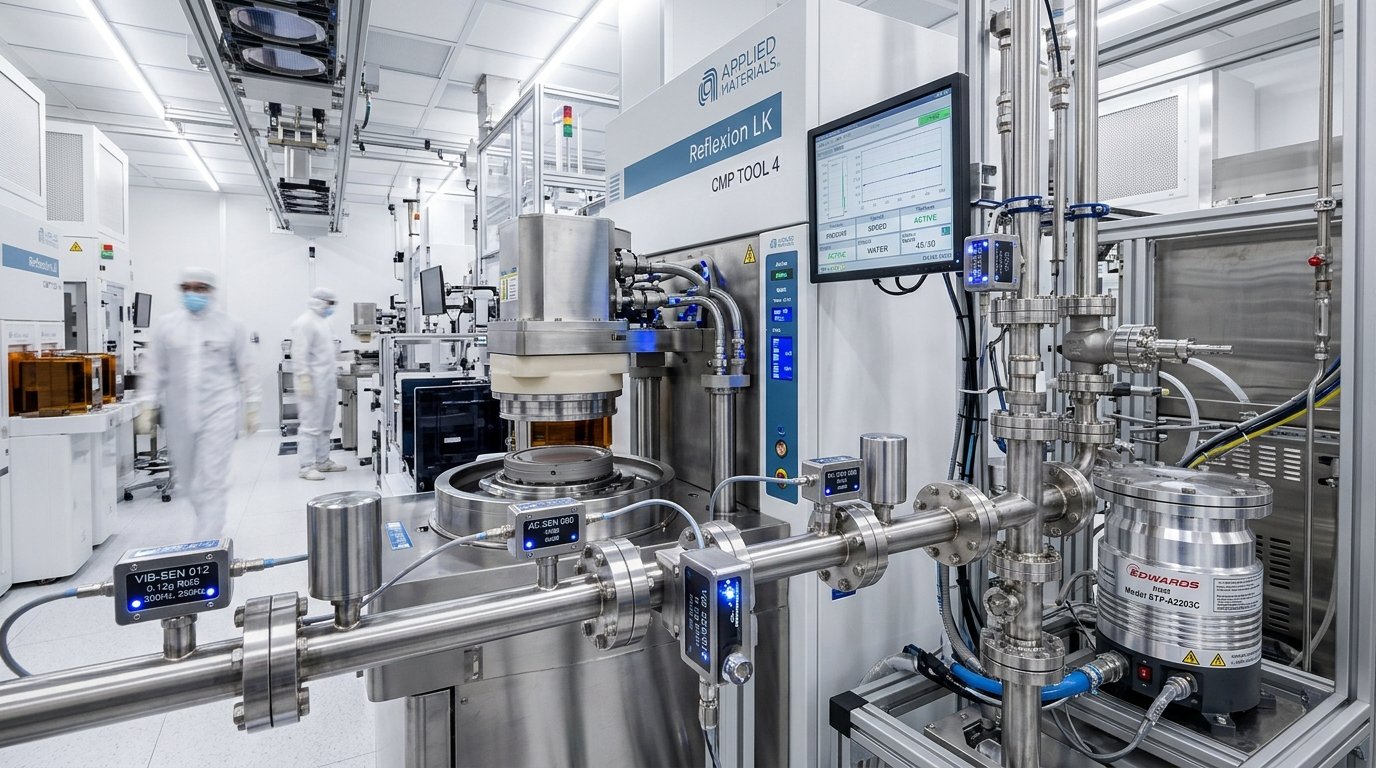
Turbomolecular vacuum pumps spinning at 60,000–90,000 RPM (up to 1,500 Hz shaft rotation) in the sub-fab maintain ultra-high vacuum for EUV/DUV lithography, etching, and PVD chambers. Even slight magnetic bearing unbalance or ceramic bearing spalling risks severe rotor damage. Our wideband 20 Hz – 10 kHz acoustic audio transducers track acoustic bearing-friction trends and mechanical wear indicators.
Chemical Mechanical Planarization (CMP) tools require nanometre-level planarity across 300mm silicon wafers. Slurry delivery line pulsation, peristaltic pump cavitation, and platen drive spindle bearing wear cause micro-scratches that degrade wafer yield. Clamp-on acoustic and vibration monitoring of slurry pumps and manifolds (no wetted contact) tracks pump health and platen vibration.
Modern lithography tools require stringent floor vibration baselines, referencing VC-E (3.12 µm/s RMS) / VC-F (1.56 µm/s RMS) criteria. Mechanical imbalance in recirculating air handling units (AHU fans), chiller water pumps, or automated overhead wafer tracks (OHT / FOUP rails) directly transfers through raised cleanroom floors. IGFO-100 tracks low-noise floor vibration trends continuously.
Fab IT policies often restrict wireless and cloud connections. The XTR 315 gateway (Launch Q3 2027) aggregates Single Pair Ethernet (SPE) cleanroom sensor channels and publishes telemetry over OPC UA and EDA / Interface A (SEMI standards support) directly into the fab's internal MES and tool host software.
| Technical Factor | Specification | Cleanroom Benefit |
|---|---|---|
| Enclosure Materials | 316L Electropolished Stainless / Hard Anodized AL | Low outgassing, non-magnetic, low particle shedding |
| Cleanroom Compatibility | Designed for use in ISO 14644-1 Class 3–4 Cleanrooms | Safe for installation directly adjacent to wafer tracks (ISO 14644-14 assessment planned) |
| Acceleration Resolution | 24-Bit ΣΔ Low-Noise Floor | Tracks vibration baseline shifts against VC curves for lithography isolation |
| Pump & Valve Audio Band | 20 Hz – 10 kHz Acoustic Audio Transducer | Detects mechanical pump wear, valve cycling acoustics, and cavitation signatures |
| Cabling Architecture | Single Pair Ethernet (SPE) / Fluoropolymer Jacketing | Chemical-resistant jacket, minimal cable bundle tray weight |
Request a cleanroom evaluation package with 316L stainless steel Mercury Z1 probes (pilot), low-noise IGFO-100 nodes, and fab SCADA test configs.